

HP MJF 3D Printing
MJF 3D PrintingHP MJF 3D Printing
Multi Jet Fusion (MJF)
MJF 3D Printing
HP MJF 3D Printing
Multi Jet Fusion (MJF)
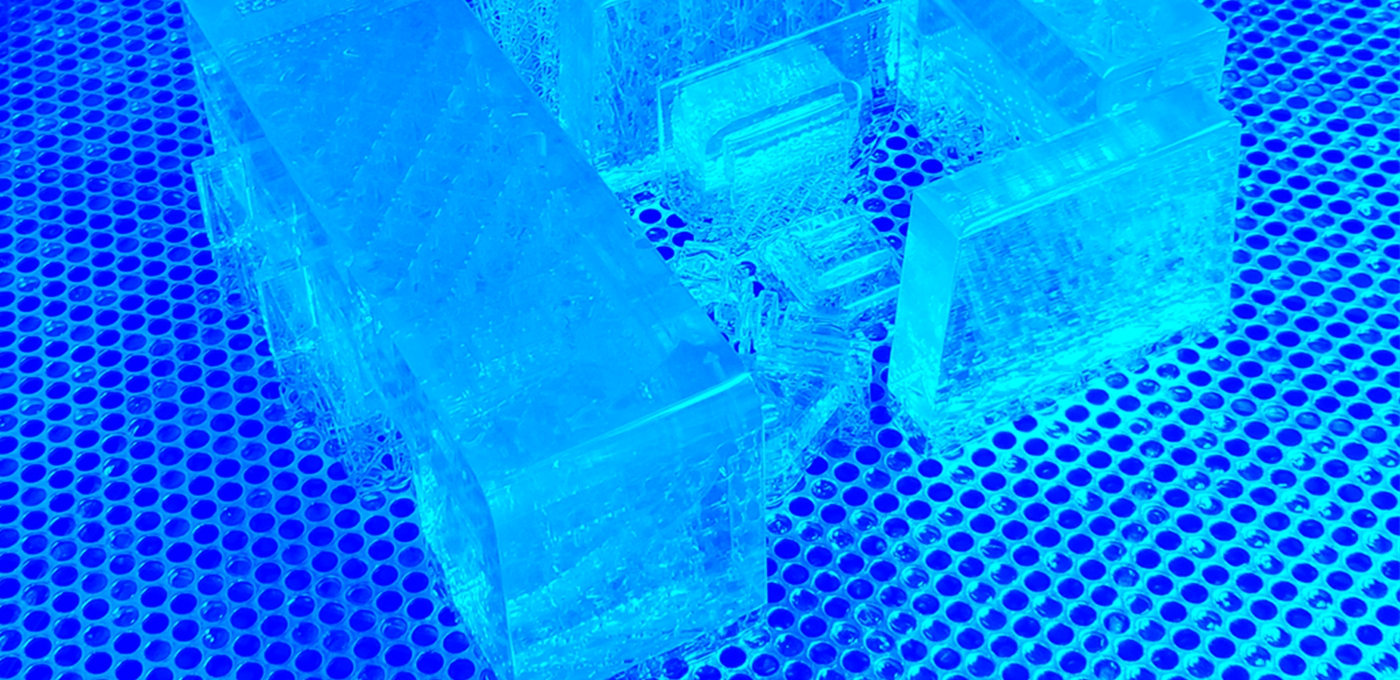
Multi Jet Fusion is an industrial 3D printing process that produces functional nylon prototypes and end-use production parts in as fast as 1 day. Final parts exhibit quality surface finishes, fine feature resolution, and more consistent mechanical properties when compared to processes like selective laser sintering.

How Does Multi Jet Fusion Work?
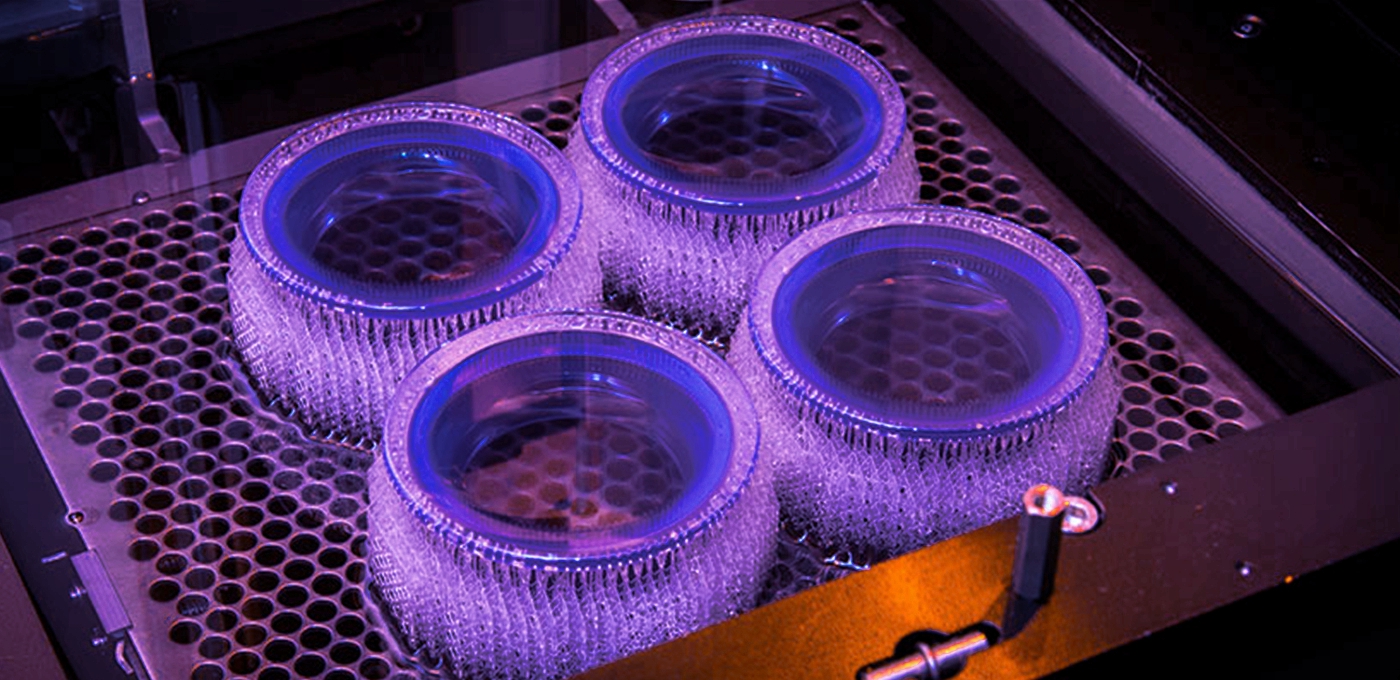
Multi Jet Fusion uses an inkjet array to selectively apply fusing and detailing agents across a bed of nylon powder, which are then fused by heating elements into a solid layer. After each layer, powder is distributed on top of the bed and the process repeats until the part is complete.
When the build finishes, the entire powder bed with the encapsulated parts is moved to a processing station where a majority of the loose powder is removed by an integrated vacuum. Parts are then bead blasted to remove any of the remaining residual powder before ultimately reaching the finishing department where they are dyed black to improve cosmetic appearance.
Why choose Multi Jet Fusion?
Multi Jet Fusion uses a fine-grained materials that allows for ultra-thin layers of 80 microns. This leads to parts with high density and low porosity, compared to parts produced with Laser Sintering. It also leads to an exceptionally smooth surface straight out of the printer, and functional parts need minimal post-production finishing. That means short lead times, ideal for functional prototypes and small series of end-parts.

Ideal applications for Multi Jet Fusion
1.Low-volume production of complex end-use parts
2.Prototypes for form, fit and function testing
3.Prototypes with mechanical properties to rival those of injection-molded parts
4.Series of small components as a cost-effective alternative to injection molding
Multi Jet Fusion Materials:
HP 3D High Reusability PA-12 Nylon
HP 3D High Reusability PA-12 Glass Beads Nylon
HP 3D High Reusability PA-11 Nylon
Ultrasint TPU 90A-01
BASF Polypropylene (PP)
Technical Specifications
Standard lead time | Minimum of 4 working days, depending on part size, number of components and finishing degrees |
Standard accuracy | ±0.3% (with a lower limit on ± 0.3 mm) |
Layer thickness | 0.08 mm |
Minimum wall thickness | 1 mm, but living hinges are possible at 0.5 mm |
Maximum build dimensions | 274 x 370 x 380 mm |
Surface structure | Unfinished parts typically have a smooth surface, without visible layers, and a stone-grey color. Multi Jet Fusion parts can be sandblasted and colored/impregnated. |
HP MJF Machine Technical Specification:
| Effective building volume | 15" x 11.2" x 15" (380 x 284 x 380 mm), bigger parts are possible with glue bonding |
| Layer thickness | 0.003" (0.08 mm) |
| Resolution | Minimum feature size of 0.020 in. (0.5mm) |
| Standard Accuracy | +/-.012" up to 4" and +/-.003" for every inch over that |
| Finish | MJF parts are a light gray color directly off the machine after post processing, our standard finish is to dye parts black |
| Building speed | 251 in³/hr (4115 cm³/hr) |
| Print resolution (x, y) | 1200 dpi |
| Software | Materialise Magics with Build Processor for MJF |
MJF & SLS: what is the difference?
HP's Multi Jet Fusion (MJF) and Selective Laser Sintering (SLS) are two industrial 3D Printing technologies that belong to the powder bed fusion family. In both processes, parts are built by thermally fusing (or sintering) polymer powder particles layer-by-layer. The materials used in both MJF and SLS are thermoplastic polymers (usually Nylon) that come in a granular form.
The main difference between MJF and SLS is the heat source. SLS uses a laser to scan and sinter each cross-section, while in MJF an ink (fusing agent) is dispensed on the powder that promotes the absorption of infrared light. An infrared energy source then passes over the building platform and fuses the inked areas.
Both MJF and SLS are capable for producing functional parts with good dimensional accuracy, smooth surface and free-form geometry.
The physical properties and mechanical behaviour of SLS materials is well-documented, but comprehensive data for MJF are not widely available.
The cost of MJF and SLS is similar, but the MJF lead time is on average 3 days faster.

MJF is a combination of the SLS and Binder Jetting technologies.
Since MJF and SLS create parts that are very similar, it is important for a designer to understand what slight differences should be expected when placing an order with either process. In this article, we compared the two technologies in terms of workflow, accuracy, materials, cost and lead time.
Fabrication process & workflow
Here is a summary of the fabrication process for the two technologies:
1.Fabrication process & workflow
Selective Laser Sintering:
A thin layer of powder is first spread over the build platform. A CO2 laser then scans each cross-section, sintering the powder. The platform then moves downwards one layer and the process repeats until the job is complete. The whole bin has to cool before the parts can be removed from the powder.
Multi Jet Fusion:
A thin layer of powder is first spread over the build platform where it is heated to a near-sintering temperature.
A carriage with inkjet nozzles (which are similar to the nozzles used in desktop 2D printers) passes over the bed, depositing fusing agent on the powder. At the same time a detailing agent that inhibits sintering is printed near the edge of the part.
A high-power IR energy source then passes over the build bed and sinters the areas where the fusing agent was dispensed while leaving the rest of the powder unaltered. The process repeats until all parts are complete.
Similar to SLS, the printed parts are encapsulated in powder and need to cool down before they can be removed.

2.Dimensional accuracy
Both MJF and SLS are industrial technologies that offer high dimensional accuracy. However, MJF has a small edge over SLS as can be seen in the table below.
This is mainly because MJF printheads deposit material at 1200 DPI (or approximately 1 dot every 0.022 mm), while the typical laser spot size of SLS system is approximately 0.3 - 0.4 mm in diameter. Also, the detailing agent used in MJF helps with printing small features and sharp edges.
Notably, neither technologies require support structures, allowing the creation of free-form models without any support removal marks, and are both susceptible to warping, so large flat areas must be avoided. In our testing, we experienced that MJF parts were more prone to warping than parts printed with SLS.
* : The recommended minimum wall thickness of structural areas for both technologies is 1 mm.
 3.Appearance & Surface Quality
The fusing agent currently used in MJF systems is black in color because dark materials absorb radiation more effectively. As a result, MJF parts have a light grey appearance. An optional post-processing dyeing step can be applied to achieve an uniform black finish.
SLS parts are usually printed white and can be dyed to any color. Grey SLS nylon powder is also available and parts printed in this material have a very similar look to MJF parts but are smoother to the touch.
Parts printed in both technologies have a grainy surface finish, but can be post-processed to a very high standard. If aesthetic appeal is the main requirement, dying is highly recommended.

4.Material Properties
The main material used in both processes is PA 12 (nylon). When printing in this material, MJF parts have superior strength and flexibility and more homogeneous mechanical properties compared to SLS parts, which are weaker along the print direction.
However, SLS printers offer more material options, such as carbon filled PA, aluminium filled PA (alumide) and flexible TPU. Moreover, SLS is a well-established and well-studied process. The properties of SLS materials are thoroughly documented by both manufacturers and independent researchers.
On the other hand, only PA is currently available in MJF and important engineering properties, such as impact strength and creep characteristics, are not widely available. Of course, this is expected to change as the technology matures and because MJF is an open material platform, allowing for faster material development.
5.Cost & Lead Time
To assess the two technologies in terms of cost and lead time, we run a small experiment on the 3D Hubs platform.
We requested quotes from 3D print services in the US for each technology, for a prototype (1 part) and for a small-batch production run (10 and 100 parts). The model used in this test was the bracket pictured below. It has a volume of 23.8 cm3 and bounding box dimensions of 101.9 x 45.0 x 18.0 mm.
MJF has the upper hand compared to SLS when it comes to pricing. It is consistently more cost-effective by approximately 15% to 30%. The price difference is smaller for larger quantities. This is probably due to the streamlined post-processing workflow (cooling, powder removal etc) available for MJF, which allows the service providers working with these systems to drop their prices.
So, is MJF the superior process? Not always. SLS offers a larger material selection including carbon and glass filled nylon, as well as TPU and PP.



 复制产品链接
 长按图片保存/分享
询盘
咨询表单:
咨询内容:
你还没有添加任何产品

询盘
咨询表单:
咨询内容:
你还没有添加任何产品
86-13143415646
Contact:
 Tel: 86-755-23000620 Fax: 86-755-23000621
 Email:info@galaxy3dm.com/info@seetoptech.com
 Address: A3 , Dingfeng Industrial Zone, Fuyong Town, Shenzhen, China
Galaxy 3D Manfacturing Solution
Copyright (©) 2020 Shenzhen Seetop Technology Co.,Limited
